Learn how to select CNC tools that reduce burrs, improve edge finishing, and maintain machining accuracy with practical tool selection and setup tips.
How to Select Elevate Tools for Better Edge Finishing and Burr Control
Burrs and rough edges can reduce part quality, create assembly problems, and add extra finishing time. A thoughtful elevate tools strategy starts with choosing the right cutter, setting stable machining conditions, and inspecting the finished edge. For CNC operators, these steps can improve consistency without relying on excessive manual deburring.
Why Burr Control Matters
A burr is unwanted material left along an edge after cutting, drilling, milling, or turning. It can affect dimensions, make parts difficult to handle, and interfere with assembly. Burr formation depends on the workpiece material, tool sharpness, cutting direction, feed, speed, and part geometry.
Suitable CNC tools help remove material cleanly, but no cutter eliminates every burr in every operation. The goal is to control burr size and location, then use a planned finishing process where needed. This can reduce rework and make inspection more predictable.
Choose the Right Tool for the Operation
Start by matching the cutter to the material and feature being machined. CNC cutting tools should be selected according to the operation—milling, drilling, turning, grooving, or chamfering—as well as the required tolerance and surface finish. Check the toolmaker’s recommendations for cutting speed, feed rate, depth of cut, and coolant use.
For edges that need a consistent bevel, a chamfer mill or countersink may be suitable, depending on the feature and material. For holes, a correctly selected deburring tool can remove sharp edges without damaging the bore. Precision cutting tools with suitable geometry and sharp edges can help maintain dimensions and reduce unwanted material at the edge.
Tool condition matters just as much as tool type. A worn or chipped edge may rub rather than cut, creating heat, poor finish, and larger burrs. Inspect cutters regularly and replace or recondition them when wear begins to affect part quality. A stable elevate tools process should include both tool selection and routine inspection.
CNC Tools for Aluminum Machining
Aluminum is relatively soft, but it can stick to the cutting edge and form built-up material. This can damage the surface finish and contribute to burrs. For milling, polished carbide end mills with sharp edges and high-helix flutes are often effective because they shear material cleanly and help evacuate chips. Two- or three-flute designs can be useful when extra flute space is needed for chip removal.
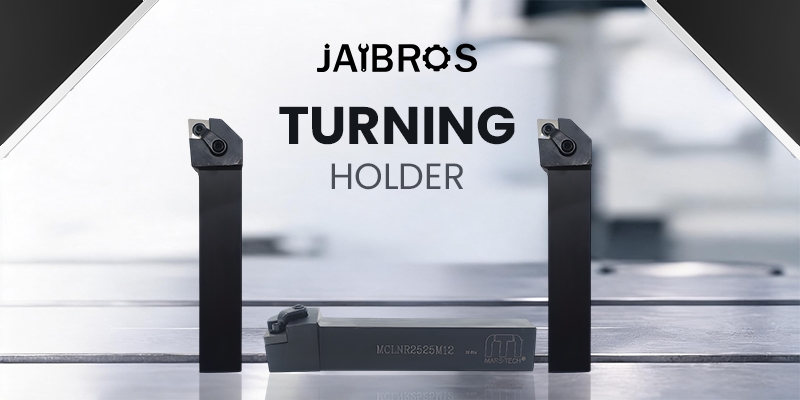
For drilling, choose a sharp drill designed for aluminum and make sure chips can leave the hole efficiently. For accurate holes, a reamer or boring tool may be appropriate after drilling, depending on the tolerance and finish requirements. During turning, a sharp insert designed for non-ferrous materials can reduce cutting forces and help produce a cleaner edge.
Select industrial cutting tools based on the aluminum alloy, machine rigidity, tool overhang, and job requirements. Use recommended cutting parameters and a suitable coolant or manufacturer-approved dry-cutting method. Avoid allowing chips to recut against the finished surface. The right elevate tools choice depends on the application, so validate settings on a sample part before full production.
Setup and Parameters Affect Edge Quality
Even good CNC machining tools can produce burrs when the setup is unstable. Secure the workpiece properly, keep tool overhang as short as practical, and check the holder, collet, and spindle for runout or damage. Vibration can leave chatter marks and inconsistent edges, while excessive heat can accelerate tool wear.
Adjust feeds and speeds using the toolmaker’s guidance rather than changing several settings at once. Inspect a test part after each controlled adjustment. These habits support machining accuracy and make it easier to identify the cause of a finishing problem. A simple elevate tools checklist can help operators verify workholding, tool condition, and cutting parameters before production begins.
Improve Cutting Tool Performance Over Time
Track recurring issues such as burrs on one side of a part, rough edges after a tool change, or a gradual decline in surface finish. Their patterns can point to tool wear, an unsuitable cutting direction, poor chip evacuation, or weak workholding. Record successful settings so repeat jobs can begin from a reliable baseline.
A practical elevate tools routine includes checking the first finished part, measuring critical dimensions, and inspecting edges under good lighting. If burrs persist, review the tool geometry and machining sequence before adding a more aggressive manual finishing step. Suppliers such as Jaibros can help manufacturers compare available cutters and specifications, but final selection should always match the material, machine, and operation.
Conclusion
Consistent edge finishing comes from combining a suitable cutter, a rigid setup, controlled cutting parameters, and regular inspection. Treat elevate tools decisions as part of the whole machining process rather than a single product choice. With careful testing and maintenance, manufacturers can reduce burrs, protect surface quality, and achieve more repeatable results.