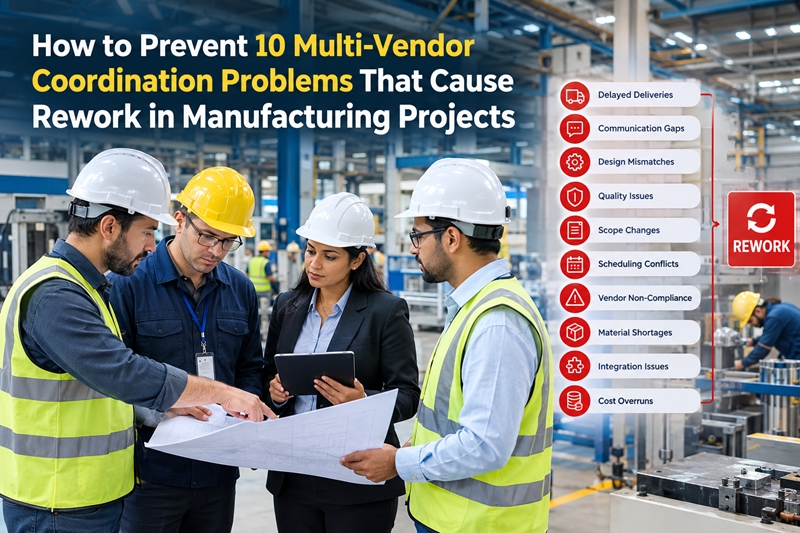
A manufacturing project can have experienced equipment suppliers, capable contractors and approved drawings, yet still suffer costly rework. The reason is often not a failure within one vendor's scope. It is the gap between scopes.
An equipment OEM may complete its machine correctly, while the civil team has built the wrong foundation interface. An automation vendor may configure the PLC correctly, while another supplier uses incompatible communication requirements. A machine may arrive on schedule, but the utilities, cabling or downstream equipment may not be ready.
These are multi-vendor coordination problems. They become expensive when they are discovered after fabrication, installation or commissioning has already started.
PMI research on engineering interfaces identifies ineffective interface management as a contributor to cost overruns, schedule slippage, commissioning delays and rework.
Why Multi-Vendor Projects Develop Rework
In a single-vendor package, responsibility may be relatively straightforward. A manufacturing plant, however, can involve equipment OEMs, civil contractors, electrical contractors, automation specialists, piping contractors, utility suppliers and commissioning teams.
Each party may have a clearly defined scope, but the connections between those scopes still need to be managed.
Typical interfaces include:
Equipment and civil foundations
Equipment and process piping
Electrical power and machine panels
PLC, SCADA and DCS systems
Equipment and plant utilities
Upstream and downstream production equipment
Vendor drawings and construction drawings
Equipment delivery and installation sequence
FAT, SAT and integrated commissioning
Rework can therefore begin with something as simple as an incorrect dimension, missing utility requirement or unresolved responsibility.
Recent ASCE research found that actual field rework averaged 0.38% of contract value before completion in the projects studied, increasing to 0.76% when estimated post-completion corrections were included. The study also found that rework was substantially underreported. These figures are not a universal manufacturing benchmark, but they demonstrate why even apparently small amounts of rework deserve systematic control.
10 Multi-Vendor Coordination Problems and How to Prevent Them
1. Unclear Scope Boundaries Between Vendors
One of the most common problems occurs when two vendors each assume that the other is responsible for an interface.
For example, an equipment supplier may provide a machine and define its electrical load, but the contract may not clearly establish who supplies the final cable, termination, isolator, communication connection or local interface panel.
The gap may remain unnoticed until installation.
How to prevent it:
Create a scope and interface matrix before execution. For every major package, identify:
What the vendor supplies
What the vendor excludes
Physical connection points
Utility requirements
Electrical responsibilities
Control-system responsibilities
Testing responsibility
Final acceptance responsibility
Do not allow phrases such as “by others” to remain undefined.
PMI recommends identifying interface boundaries between work packages and establishing how affected parties will exchange information and resolve interface issues.
2. Vendor Drawings Arrive Too Late
A machine can be ordered months before installation, but its final engineering information may still be evolving.
Late information about equipment dimensions, foundation loads, nozzle locations, electrical loads or utility requirements can force downstream teams to modify work that has already started.
How to prevent it:
Create a vendor document schedule linked to project milestones.
Track:
Drawing submission
Engineering review
Comments
Revision
Approval
Approved-for-construction status
Downstream impact
The important distinction is that equipment delivery and engineering readiness are not the same milestone.
If civil construction needs an approved foundation drawing by 10 March, the vendor's obligation should be tied to that engineering need, not merely to the equipment delivery date.
3. Every Vendor Has a Schedule, but the Project Has No Integrated Schedule
Suppose three suppliers report:
Machine A ready: 15 June
Machine B ready: 18 June
Packaging system ready: 20 June
That sounds manageable.
But if power is available on 25 June, controls are ready on 28 June and integrated testing starts on 2 July, the individual vendor schedules do not tell the real project story.
How to prevent it:
Build one master schedule around system readiness, not only vendor milestones.
Track the sequence:
Engineering → Procurement → Delivery → Installation → Utilities → Electrical → Controls → Testing → Integration → Production trial
A vendor should not be considered “complete” simply because its equipment has arrived. The relevant question is:
Can this equipment now participate in the next planned project activity?
4. Equipment From Different Vendors Is Technically Incompatible
Multi-vendor integration can fail even when every individual system works correctly.
Examples include differences in:
Communication protocols
Data structures
I/O requirements
Voltage levels
Utility pressures
Flow requirements
Control philosophy
Mechanical connection standards
NIST research has specifically identified interoperability challenges in manufacturing systems built from multiple vendor technologies. Incompatible representations and formats can create additional integration work and prevent systems from operating together as intended.
How to prevent it:
Define interface requirements before purchase orders are finalized.
For critical equipment, review:
Mechanical interfaces
Electrical interfaces
Instrumentation
PLC/SCADA/DCS communication
Data exchange
Interlocks
Safety signals
Utility requirements
I/O mapping
Compatibility should be demonstrated during engineering and testing, not discovered during start-up.
5. Nobody Owns the Interface Between Two Vendors
A project may know that two systems need to communicate but still fail to assign responsibility for making that communication work.
Consider a filling machine and packaging machine. Who defines the handshake signals? Who provides the communication cable? Who configures the PLC? Who tests the sequence? Who signs off the result?
If the answer is “both vendors,” the interface may remain unresolved.
How to prevent it:
Create an interface register containing:
Interface | Responsible Party | Supporting Vendor | Due Date | Closure Evidence |
|---|---|---|---|---|
Machine power | Electrical lead | OEM | 10 Aug | Energization record |
PLC communication | Automation lead | OEM | 15 Aug | Integration test |
Utility connection | Project engineering | Process vendor | 18 Aug | Test record |
Production handshake | System integrator | Two OEMs | 25 Aug | SIT record |
An interface should be considered closed only when the required evidence exists.
6. A Change Reaches One Vendor but Not the Others
A change to equipment location may appear minor until its effects reach piping, electrical, HVAC, automation and civil works.
If only one affected contractor receives the revision, different teams can continue working from different assumptions.
How to prevent it:
Use formal change control.
Every significant change should identify:
What changed?
Why did it change?
Which vendor initiated it?
Which systems are affected?
Which drawings must be revised?
What is the cost impact?
What is the schedule impact?
Who must approve it?
What evidence confirms implementation?
ISO's quality-management guidance emphasizes controlling changes and ensuring current document revisions are identified and available where needed.
Speak With An Expert: https://www.imarcengineering.com/contact?service=multi-vendor-coordination-and-integration
7. Different Vendors Work From Different Drawing Revisions
Imagine the equipment OEM has issued GA drawing Rev. 05, while the civil contractor is working from Rev. 03 and the electrical team has Rev. 04.
Each team may believe it is following approved information.
The result can be:
Incorrect foundation openings
Wrong equipment locations
Misaligned cable routes
Incorrect piping connections
Repeated fabrication
How to prevent it:
Maintain a controlled document register with:
Document number
Current revision
Approval status
Date issued
Recipient
Superseded revision
Required action
Document control is not merely administrative. ISO guidance specifically emphasizes revision status, controlled distribution and preventing unintended use of obsolete information.
8. Vendors Optimize Their Own Equipment Instead of the Complete Production Line
A machine can meet its individual specification and still fail to meet the plant's production objective.
For example, one machine may operate at a higher rate than the upstream process can supply. Another may discharge products faster than the downstream packaging system can accept them.
The equipment is technically successful. The production system is not.
How to prevent it:
Define system-level requirements before accepting individual equipment.
Review:
Line throughput
Cycle time
Buffer requirements
Product transfer
Interlocks
Changeover sequence
Reject handling
Upstream/downstream dependencies
Overall performance criteria
NIST notes that systems engineering coordinates multiple disciplines so that the resulting system meets overall requirements rather than isolated discipline objectives.
9. Vendor Commissioning Is Planned Separately
A vendor may successfully commission its machine without proving that the machine works with the rest of the plant.
This creates the familiar situation:
Machine A works.
Machine B works.
PLC works.
Utilities work.
Production line does not.
The missing activity is integrated testing.
How to prevent it:
Define testing responsibilities before site commissioning.
For automation systems, IEC 62381:2024 covers Factory Acceptance Testing (FAT), Factory Integration Testing (FIT), Site Acceptance Testing (SAT) and Site Integration Testing (SIT), and emphasizes agreement between owner, buyer and vendor on test scope and responsibilities.
The project should therefore progress from:
Equipment testing → subsystem testing → integration testing → production trial → performance verification
10. There Is No Central Authority for Cross-Vendor Issues
This is where coordination can break down completely.
One vendor blames the PLC. The automation contractor points to the machine interface. The electrical contractor says its installation matches the approved drawing.
Everyone may be correct within their individual scope.
But the plant still does not operate.
How to prevent it:
Assign a central project function responsible for cross-vendor interfaces.
That function should:
Maintain the interface register
Coordinate technical decisions
Track open issues
Assign owners
Escalate overdue actions
Assess cross-vendor impacts
Coordinate testing
Confirm closure
The objective is not to replace each vendor's technical responsibility. It is to ensure that someone owns the system-level outcome.
A Practical Multi-Vendor Coordination Checklist
Before installation or commissioning, confirm:
Vendor scope boundaries are documented
Interface responsibilities are assigned
Critical vendor drawings are approved
Latest drawing revisions are controlled
Equipment loads and utility requirements are confirmed
Electrical and instrumentation interfaces are defined
PLC/SCADA/DCS communication requirements are agreed
Vendor schedules are linked to the master project schedule
Changes are formally reviewed for downstream impact
FAT/SAT/SIT responsibilities are defined
Open interface issues have named owners
Integrated performance requirements are established
This checklist is more useful than simply asking whether each vendor is “on track.”
The Key Shift: Track Interface Readiness, Not Just Vendor Readiness
A useful way to manage multi-vendor projects is to distinguish vendor readiness from interface readiness.
A machine might be:
100% manufactured
100% delivered
100% installed
Yet its interface readiness may still be:
0%
if power, utilities, communication, upstream/downstream integration or safety interlocks are unresolved.
That distinction changes how project teams monitor progress.
Instead of asking:
“Has the vendor completed its work?”
ask:
“Can this package now connect, operate and be tested with the systems around it?”
That is the level at which manufacturing projects actually become operational.
How IMARC Engineering Can Help
IMARC Engineering can support multi-vendor manufacturing projects by coordinating technical interfaces, vendor deliverables, integrated schedules and cross-functional dependencies. Its coordination approach can cover scope alignment, document tracking, vendor communication, interface issue resolution, installation readiness and commissioning integration. The objective is to identify gaps before they become site rework, prevent disconnected vendor schedules from affecting the master plan, and help project teams move from individual equipment completion toward integrated plant readiness.
Conclusion
Multi-vendor rework is rarely caused by the number of suppliers alone. It grows when interfaces, responsibilities, technical information, changes and commissioning activities are left uncoordinated. A practical system of interface registers, controlled documents, integrated schedules, defined responsibilities and system-level testing can identify many problems before they reach the site. The most important question is therefore not whether every vendor has completed its scope, but whether all vendor scopes work together as one functioning manufacturing system.
Contact Us:
IMARC Engineering
Phone: +91-120-433-0800
Email: sales@imarcengineering.com
India: C-130, Sector 2, Noida, Uttar Pradesh 201301
LinkedIn: https://www.linkedin.com/showcase/imarc-engineering/